Punch more holes with PVD-coated punches.
Presses always down to sharpen or replace punches? Reduce tooling maintenance and press downtime with PVD-coated punches. When you're punching lots of holes, a PVD coating is a necessity for maximizing tool life and minimizing press downtime.
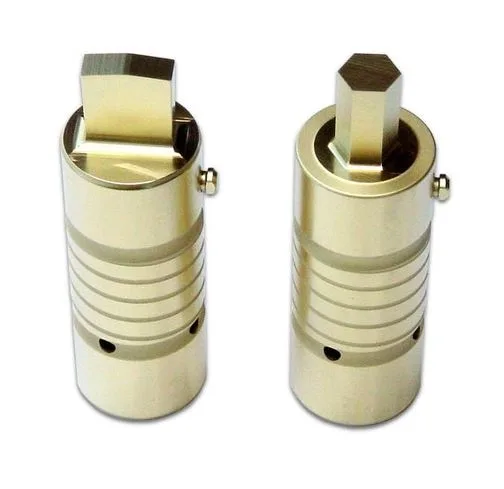
Alpha™-coated turret punches
The cutting edge wears going in — and coming back out.
When punching, the cutting edge of the punch wears as it goes into and then through the sheet metal. As the punch continues to the bottom of the stroke, wear continues at the cutting edge and down the side of the punch. As the punch is stripped from the metal sheet, the punch wears again, only in the opposite direction.
With a PVD coating, the punch edge holds up much longer and side wear and galling (metal sticking to the punch) are greatly reduced. When the punch is eventually sharpened, the coating remains on the punch sides to continue providing the same benefits over and over.
What our punching customers see once tools come back coated.
6–10× longer life
PVD-coated punches typically last 6–10 times as long as uncoated punches, dramatically reducing sharpening and changeover time.
Less pick-up, cleaner holes
The hard, low-friction surface reduces material pick-up (galling), so holes stay dimensionally accurate and finish quality improves.
More sharpenings per tool
When sharpening is required, less material has to be removed, resulting in more sharpenings per punch across its service life.
More up-time
Longer runs between sharpenings, fewer punch swaps, fewer press stops — all of which translates directly into more parts and more profit.
All five of our coatings are used on punches.
Alpha™ and TiCN are extremely hard and usually last 2–4× longer than TiN. If galling is an issue, try CrN for improved lubricity.
Alpha — maximum life
Our hardest all-purpose coating — 2–4× the life of TiN on punches. Used successfully on turret punches, pierce punches, and combination tooling.
Learn about AlphaTiCN — hard wear
~80% harder than TiN. 2–4× the tool life on demanding punches and heavier stock.
Learn about TiCNCrN — anti-galling
Excellent lubricity for stainless and other galling-prone materials. The first coating we reach for when metal is sticking to the punch.
Learn about CrNWe coat most common tool steels used for punches.
A-2, D-2, M-2 and many other tool steels are routinely coated. Some customers are concerned about drawing back their tool steels during the coating process. This may happen with some materials, but it usually doesn't affect the performance of the punch if the hardness remains above 55 Rc.
Punch up more profits with a PVD coating.
Send us the punch, the material, and the sheet you're piercing — we'll recommend the right coating. Response within one business day.